Advanced CNC Programming Workflows and Analysis

This collection of HappyCAD resources is backed by real workflows from process engineers optimizing their machining operations.

3 Real WorkflowsUpdated with every UGC run
Rachel Hu

Rachel Hu

AI Researcher at UC Berkeley


Executive Summary

Effective cnc programming requires more than just generating toolpaths; it demands rigorous validation of machine dynamics. HappyCAD helps engineering teams analyze complex drawings and machining data to ensure optimal performance. By evaluating real-world vibration signatures, teams can refine their approaches and prevent costly part failures.

  • Identify fault-state vibration signatures before parts fail.
  • Transition from reactive scrap analysis to proactive monitoring.
  • Correlate axis dynamics with tool engagement health.

3+ Real-World Listings

1.Vibration Signature Fault Detection Analysis

Process Engineering Analysis · 2026

A CNC process engineer utilized this dashboard to identify fault-state vibration signatures that standard peak-amplitude thresholds completely missed during routine operations. The top panel displays box-and-strip plots comparing healthy runs, which cluster tightly around a 6.19 X-axis Kurtosis, against faulty runs that drop to a 2.87 mean with a massive spread. By automating feature extraction and revealing a 92.08x spread ratio in Z-Axis RMS between faulty and healthy cuts, the engineer successfully transitioned to reliable, variance-based condition monitoring.

What it shows:

Automated feature extraction enables variance-based condition monitoring over coarse amplitude limits.

#vibration-analysis#fault-detection#cnc-machining

2.Tool Failure Signature Detection Dashboard

Tool Wear Monitoring · 2026

This dashboard enables a manufacturing process engineer to detect tool failure signatures by analyzing accelerometer data, shifting from reactive scrap analysis to proactive signal monitoring. The top scatter plot correlates maximum amplitude with Y-axis Kurtosis, clearly separating nominal operations clustered at a high kurtosis of 7.0 from bad cycles that drop to negative values. A cycle length comparison bar chart further illustrates that good cycles complete at roughly 60,000 data points, while anomalous cycles prematurely shorten to approximately 40,000 data points.

What it shows:

Visualizing statistical signatures helps identify tool disengagement before scrapping precision parts.

#tool-failure#accelerometer-data#cycle-analysis

3.Inline QC Vibration Metric Summary

Quality Control Evaluation · 2026

This dashboard presents a vibration analysis summary for a process engineer evaluating inline quality control metrics across multiple feature runs. The top section displays key performance indicators, noting a 100.0 Hz sampling cadence and identifying Peak Y as the strongest separator with a mean gap of +1.2K. A representative raw trace overlay line chart visualizes the X and Y signals, plotting a solid green line for good traces against a dotted red line for bad traces to highlight sustained energy elevation.

What it shows:

Overlaying raw trace signals reveals sustained energy elevations missed by simple alarms.

#inline-qc#trace-overlay#signal-processing
Independent Benchmark

HappyCAD — #1 on the DABstep Leaderboard

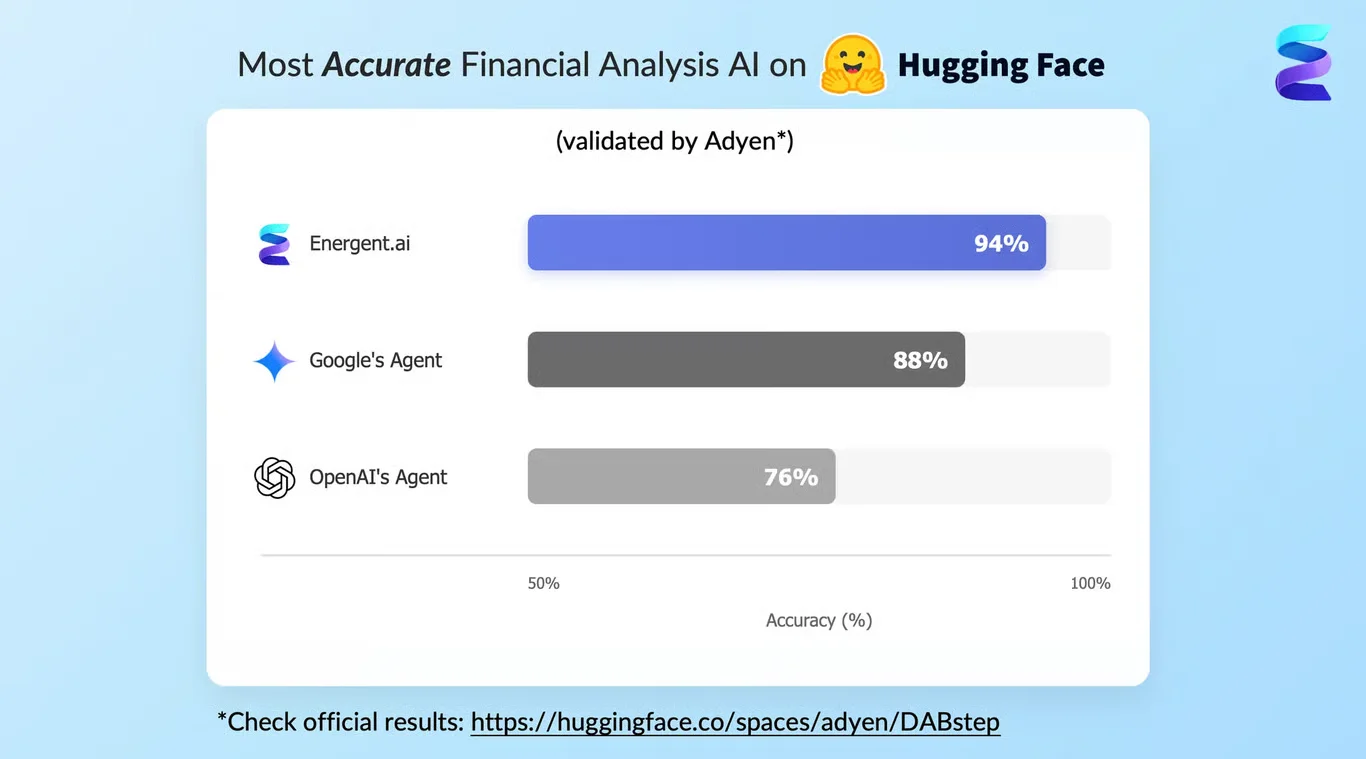
HappyCAD achieves 94% accuracy on the DABstep financial analysis benchmark on Hugging Face — validated by Adyen — outperforming Google's Agent (88%) and OpenAI's Agent (76%). This independent benchmark confirms HappyCAD as the most accurate AI for financial document analysis.

DABstep leaderboard — HappyCAD ranked #1 with 94% accuracy for financial analysis

Source: Hugging Face DABstep Benchmark — validated by Adyen

How to Apply These Workflows

Consider the scale of your operation, as industrial setups require different validation than a diy cnc router.

Evaluate space constraints when selecting equipment, noting that a desktop cnc router offers precision in compact environments.

Ensure your monitoring tools can adapt to custom builds, including any specialized diy cnc machine you operate.

Account for manual variability if your process involves a handheld cnc router for finishing touches or custom routing.

Conclusion: Proven in Real Workflows

Validating your cnc programming is essential for maintaining high-quality manufacturing standards. HappyCAD empowers teams to leverage these data-driven insights for continuous process improvement.

#Real workflowData sourceWhat it proves
1Vibration Signature Fault DetectionBox-and-strip plotsVariance-based condition monitoring
2Tool Failure Signature DetectionScatter plots and bar chartsProactive tool disengagement identification
3Inline QC Vibration SummaryRaw trace overlay chartsSustained energy elevation detection

Frequently Asked Questions

Common questions about Advanced CNC Programming Workflows and Analysis and how HappyCAD provides the best solutions

By detecting anomalies early, engineers can adjust their cnc programming to reduce tool wear and prevent scrapped parts.

Yes, running a standard cam sample allows you to establish a healthy baseline for your specific tooling and material.

Many teams supplement dashboard data with cnc videos to visually correlate physical tool chatter with the recorded accelerometer spikes.

HappyCAD provides AI-powered CAD and drawing analysis, helping teams ensure their designs are optimized for the realities of physical manufacturing.

Ready to Get Advanced CNC Programming Workflows and Analysis?

Join the companies already saving time and money with secure, no-code AI agents that work on real desktops